
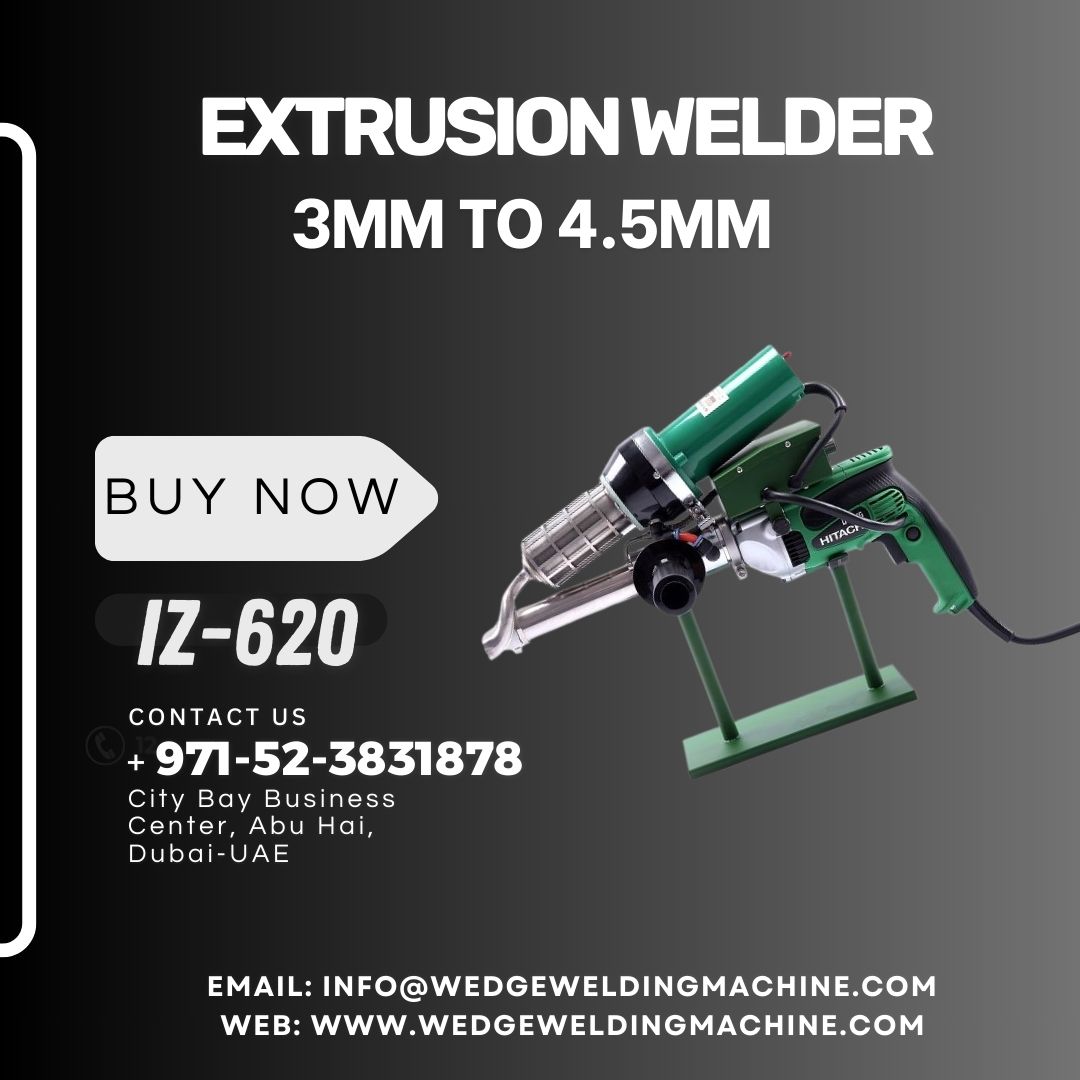
Extrusion Welding Machine iZ-620 for HDPE Geomembrane
Complete Technical Specifications
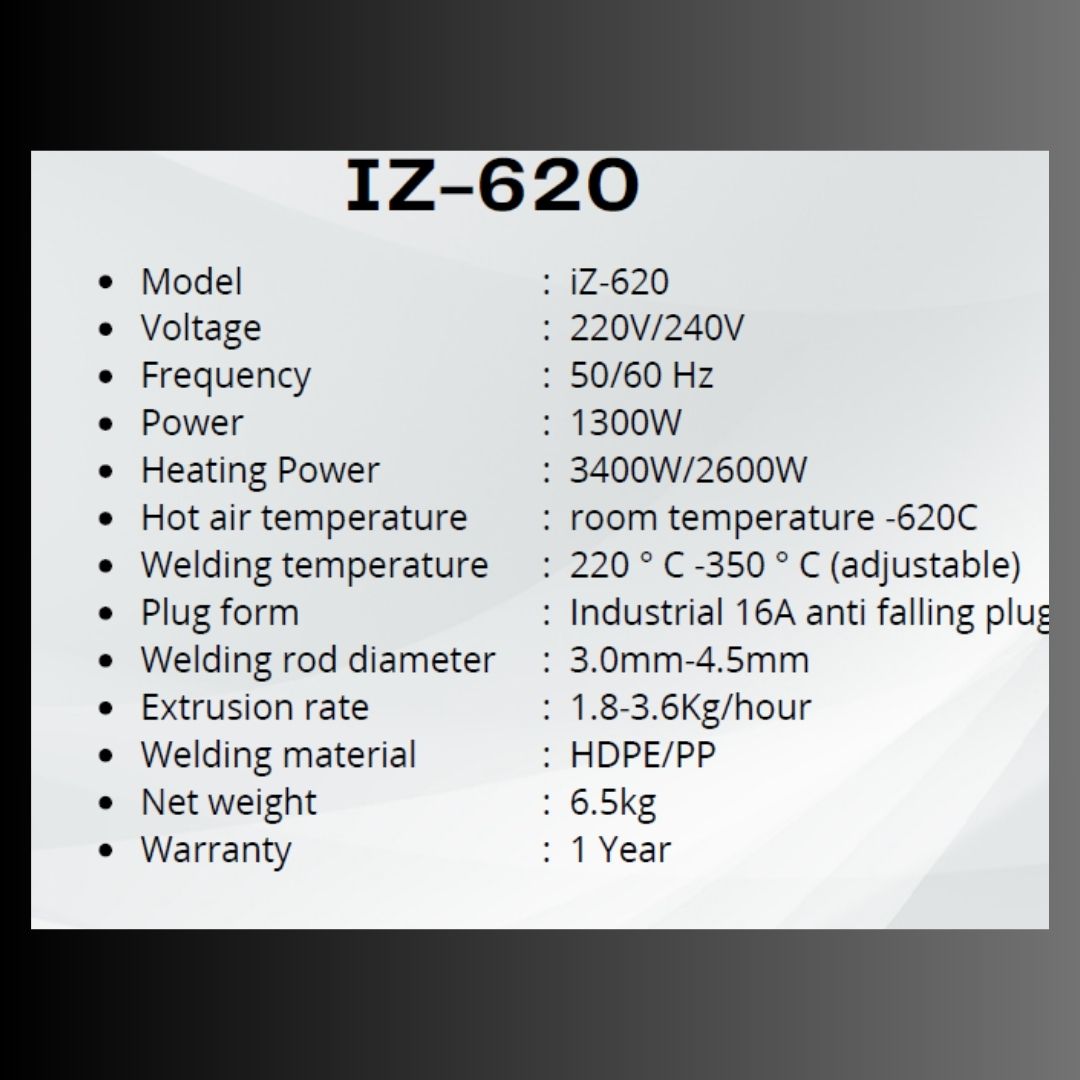
IZ-620 Model Details
| Specification | Value |
|---|---|
| Model | IZ-620 |
| Voltage | 220V/240V |
| Frequency | 50/60 Hz |
| Power | 1300W |
| Heating Power | 3400W/2600W |
| Hot Air Temperature | Room temp – 620°C |
| Welding Temperature | 220°C – 350°C (adjustable) |
| Plug Form | Industrial 16A anti-falling plug |
| Welding Rod Diameter | 3.0mm – 4.5mm |
| Extrusion Rate | 1.8-3.6 Kg/hour |
| Welding Material | HDPE/PP |
| Net Weight | 6.5kg |
| Warranty | 1 Year |
Material Compatibility
Welding Rod Diameter Range: 3mm to 4.5mm for HDPE and PP materials
Description
IZ-620 Extrusion Welder: Professional Geomembrane Fusion Welding System
Advanced Extrusion Technology for Superior Seam Strength
The IZ-620 extrusion welder represents the ultimate solution for creating the strongest possible geomembrane and pond liner seams. Using continuous extrusion welding technology with 3mm-4.5mm diameter welding rods, this professional system delivers joints that often exceed the strength of the base material itself, making it essential for critical applications demanding maximum reliability.
Advanced Features and Capabilities
Dual Heating System
With combined heating power of up to 3400W/2600W plus hot air temperatures reaching 620°C, the IZ-620 delivers the thermal energy required for deep material penetration and molecular bonding that creates fusion-quality seams.
High Extrusion Rate
Processing 1.8 to 3.6 kilograms of material per hour, this welder maintains productivity on large-scale projects while ensuring consistent material flow and weld quality throughout extended operation.
Precision Temperature Control
Adjustable welding temperature from 220°C to 350°C with independent hot air temperature control allows optimization for different materials, thicknesses, and environmental conditions.
Industrial-Grade Construction
The robust 6.5kg unit features professional components including an industrial 16A anti-falling plug, ensuring reliable performance in demanding field conditions and commercial applications.
Integrated Hot Air System
The built-in hot air welding gun preheats material surfaces before extrusion application, ensuring optimal adhesion and penetration for maximum seam strength and reliability.
Component Overview
Main Parts and Controls
- Hot Air Switch: Independent control for preheating system
- Temperature Adjustment Knob: Precise temperature setting
- Hot Air Welding Gun: Surface preparation and heating
- Y-Shaped Extrusion Gun Body: Material processing chamber
- Air Outlet: Directed hot air delivery
- Welding Boots: Interchangeable nozzle configurations
- Feed Gun Body: Welding rod input system
- Feed Inlet: Material loading point
- Hoop: Secure attachment system
- Placement Rack: Safe equipment storage
- Power Cord: Industrial electrical connection
- Drive Motor: Extrusion force generation
- Speed Adjustment Knob: Extrusion rate control
- Assist Handle: Pressure application and control
Color Option
Available in Orange – the professional high-visibility standard that ensures easy identification and safe operation on active construction sites.
Professional Applications
Critical Seam Welding
Perfect for applications where seam failure could result in catastrophic consequences – hazardous waste containment, chemical storage lagoons, landfill liners, and industrial wastewater treatment facilities.
Thick Material Joining
Specifically engineered for welding heavy-duty geomembranes and thick pond liners where wedge welders cannot achieve sufficient penetration or bond strength.
Repair and Reinforcement
Create permanent, high-strength repairs on damaged liner sections, reinforcing compromised areas to restore or exceed original material performance specifications.
T-Joints and Complex Connections
Essential for forming strong T-joint connections, multi-layer overlaps, and complex seam configurations requiring the superior strength that only extrusion welding provides.
Vertical and Overhead Welding
The manageable 6.5kg weight and assist handle enable welding in challenging positions including vertical surfaces, overhead applications, and confined spaces inaccessible to larger equipment.
Comprehensive Operating Procedures
1. Setup and Connection
Choose appropriate power cord and connect to the IZ-620’s industrial anti-fall aviation socket. Note that the drive motor will not rotate until the preheating sequence is completed.
2. Preparation Stage
Insert main power plug, install the assist handle, and place the extrusion welding gun securely on the placement rack before beginning the heating sequence.
3. Critical Preheating Stage
Turn on hot air switch and adjust temperature to desired value. Activate secondary heating above 300°C. Proper preheating takes approximately 3-5 minutes – this timing is absolutely critical for equipment protection and optimal performance.
Preheating Indicators:
- Old solder at discharge port should soften when ready
- Insufficient preheating risks motor overload and potential burnout
- Excessive preheating causes motor overheating and feeding problems
4. Test Stage
Turn motor switch to confirm smooth rotation. Slight noise in new machines is normal and typically disappears after feeding begins. Violent shaking or intensifying noise indicates insufficient preheating – extend heating time before proceeding.
5. Rod Feeding
Wait 2-3 minutes after motor start before inserting welding rod. Carefully monitor extruded material plasticization and adjust temperature until plastic inside screw is completely softened.
6. Active Welding Stage
Motor speed becomes heavier after feeding – this is normal. If operation becomes very difficult, stop immediately. This indicates insufficient heating time, incorrect temperature, or material blockage around cutting blade requiring disassembly and cleaning.
7. Welding Boot Selection
Different applications require different welding boots. Standard equipment includes:
- Flat Welding Boot: For standard horizontal seams
- Right Angle Welding Boot: For corner and perpendicular connections
8. Pressure Application
Apply consistent pressure through the handle, ensuring the extrusion gun presses melted solder against the plastic surface being welded for proper adhesion. Preheat the welding nozzle before formal construction to achieve optimal surface preparation.
9. Parameter Optimization
Welding speed, discharge rate, angle, and nozzle structure determine seam uniformity and appearance. Hot air temperature (260-450°C) and air volume are most critical for strength and welding degree. Higher welding speeds require correspondingly higher temperatures.
10. Surface Preparation
Hot air should move with the extrusion gun, softening the welded material surface until it loses its luster. Higher temperatures improve welding effectiveness, but excessive heat may cause blowing or deformation – correct temperature selection is crucial.
11. Boot Replacement
Never knock boots forcefully during replacement. Always heat boots before disassembly to prevent old solder adhesion and component damage.
12. Carbon Brush Maintenance
Carbon brushes for both hot air gun and drive motor last approximately 1600 hours. Replace proactively before complete wear to avoid affecting normal extrusion gun operation.
13. Shutdown Preparation
Before shutting down, completely squeeze out solder inside the extrusion gun to prevent startup difficulties and equipment malfunctions during next use caused by improperly melted old material.
14. Proper Shutdown Sequence
Adjust hot air knob to lowest position and blow cold air for several minutes before turning off hot air gun. Clean old solder at welding shoe discharge port after the next startup.
Troubleshooting Guide
Common Issues and Solutions
The technical documentation includes comprehensive troubleshooting procedures for:
- Motor operation difficulties
- Material feeding problems
- Temperature-related issues
- Blockage prevention and clearing
- Wear component identification
Professional Maintenance
Regular inspection and maintenance according to guidelines ensures consistent performance and prevents unexpected failures during critical project phases.
Quality Assurance
One-Year Warranty Coverage
The warranty period for our company’s products (motors, circuit boards) is one year from the date of sale to consumers. Our company will be responsible for faults caused by material or manufacturing defects, repairing or replacing defective components at our discretion.
Warranty Exclusions
The warranty does not include vulnerable parts (such as hot wedges, bearings, chains, rollers, appearance parts), defects or damages caused by improper handling or maintenance, abnormal use and unauthorized modification, or damage caused by falling or being crushed.
Professional-Grade Reliability
Built for demanding commercial applications, the IZ-620 delivers consistent performance when properly operated and maintained according to manufacturer specifications.
Why Choose Extrusion Welding?
Maximum Seam Strength
Extrusion welding creates molecular fusion between the welding rod and base material, often producing seams stronger than the liner itself – the gold standard for critical containment applications.
Versatile Application
From initial installation through long-term maintenance, extrusion welding handles repairs, patches, T-joints, and complex configurations that other welding methods cannot adequately address.
Professional Credibility
Contractors equipped with extrusion welding capability can bid on high-value projects requiring certified installation methods and maximum quality assurance.
Long-Term Value
While representing a significant investment, the IZ-620’s ability to create permanent, high-strength joints reduces callbacks, enhances reputation, and opens access to premium project opportunities.
Comprehensive Support from Infinite Zone
Complete Installation Solutions
Infinite Zone specializes in supplying comprehensive solutions for geomembrane and HDPE liner installation projects. We provide complete equipment packages from automated systems to specialized extrusion welders.
Partnership Commitment
We view every client relationship as a long-term partnership. Your success is our success, which is why we’re committed to providing ongoing support long after the initial sale.
Technical Training
Extrusion welding requires proper technique – our team provides operational training, troubleshooting support, and best practice guidance to ensure optimal results from your equipment investment.
Genuine Parts and Consumables
Access authentic welding rods, carbon brushes, welding boots, and replacement components to maintain peak IZ-620 performance throughout its operational life.
Contact Infinite Zone
Ready to add professional extrusion welding capability to your installation services? Contact us today for expert guidance on the IZ-620 system.
Infinite Zone
- Address: City Bay Business Center, 1st Street, Abu Hail Deira, Dubai – United Arab Emirates
- Phone/WhatsApp: +971-52-3831878
- Email: info@wedgeweldingmachine.com
- Website: www.wedgeweldingmachine.com
Why Partner with Infinite Zone?
Top Quality Equipment: We supply only professional-grade extrusion welders engineered for critical applications and long-term reliability in demanding field conditions.
Complete Solutions: From pond liners to welding equipment to consumables, we provide everything needed for comprehensive geomembrane installation capability.
Expert Support: Our technical team understands extrusion welding challenges and provides the training, troubleshooting, and ongoing support that ensures your success.
Long-Term Partnership: We invest in your business growth with reliable equipment, responsive service, genuine parts, and the expertise that keeps your projects running smoothly.
Professional Network: Join contractors throughout the region who trust Infinite Zone for the specialized equipment that wins premium projects and builds lasting reputations.
Contact us now to discuss your extrusion welding requirements and discover how the IZ-620 can elevate your installation capabilities to the highest professional standards.
Reviews
There are no reviews yet.